

We offer a comprehensive range of precision metal processing equipment, including straightening, cold drawing, pointing, chamfering, cutting, thread rolling machines, and drawing dies, tailored for tube, bar, and wire materials across diverse industries.
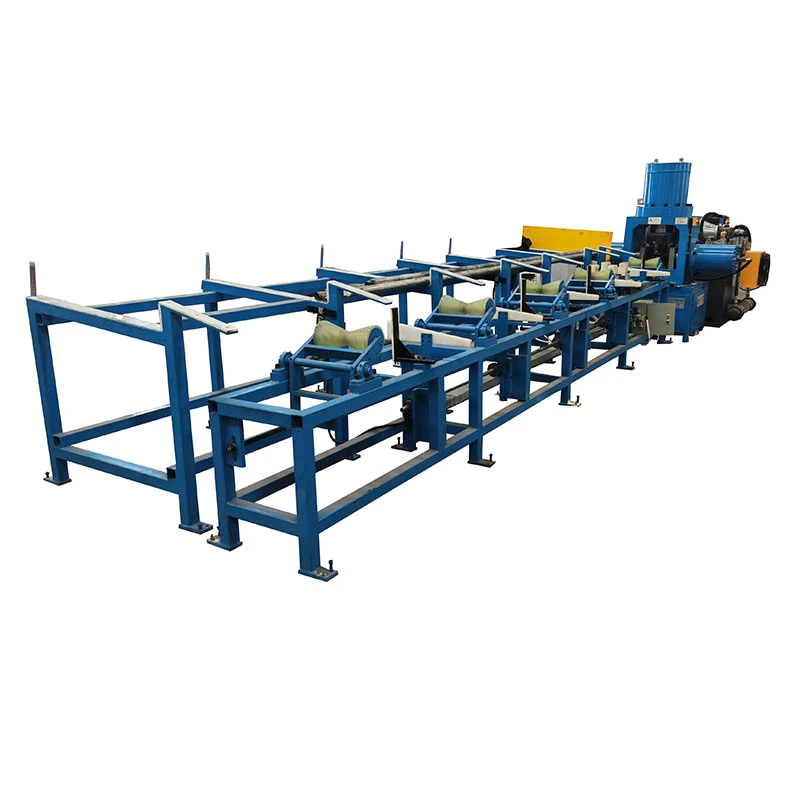
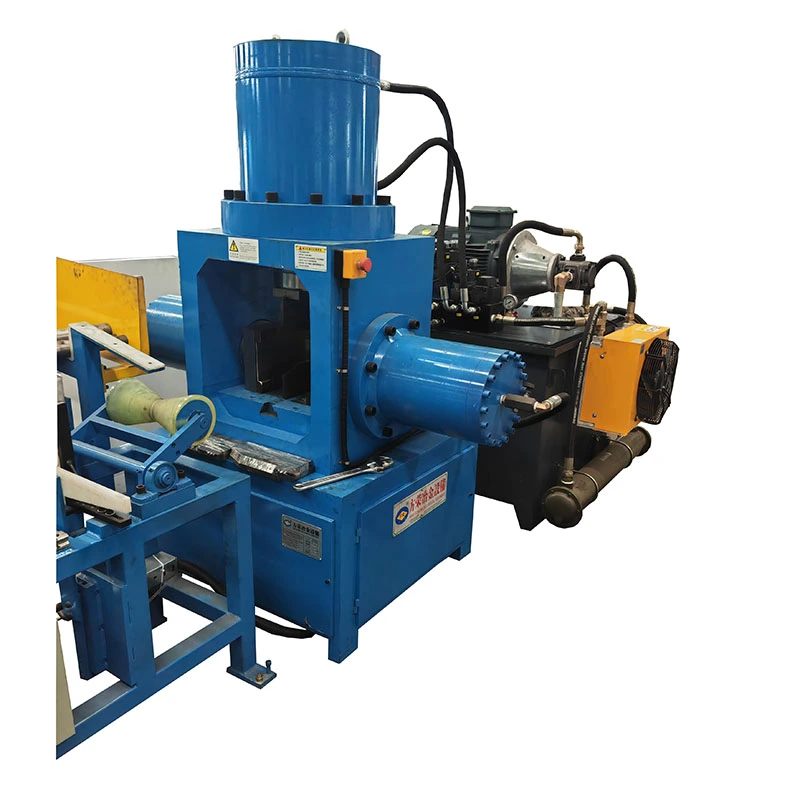
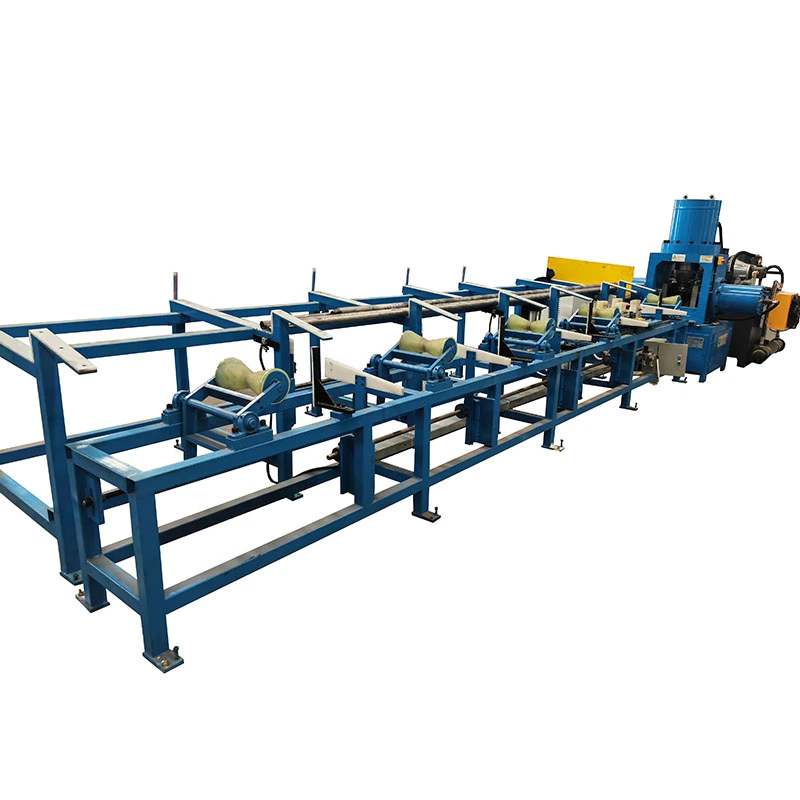
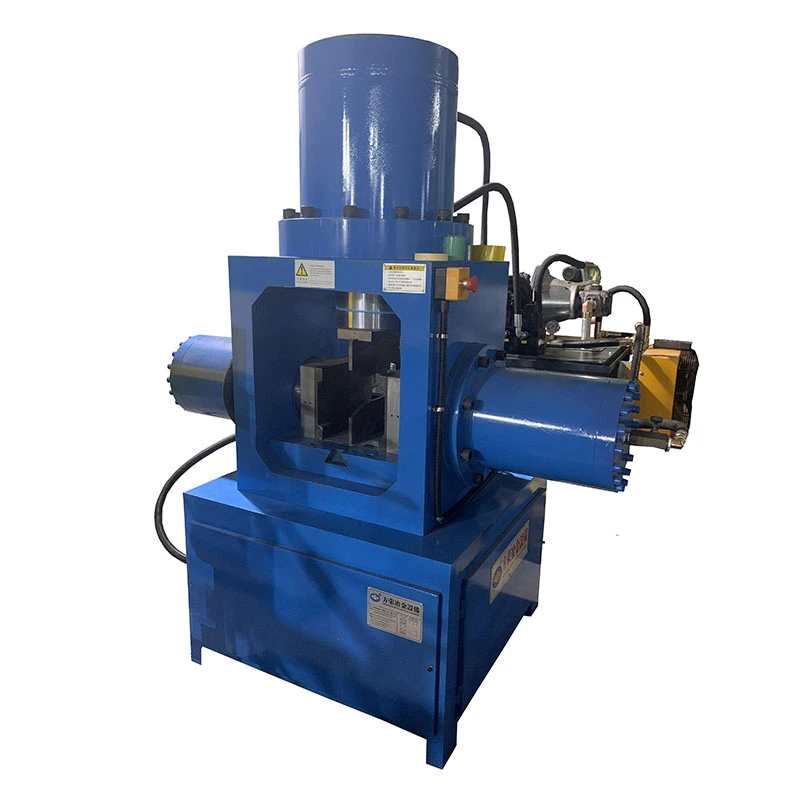
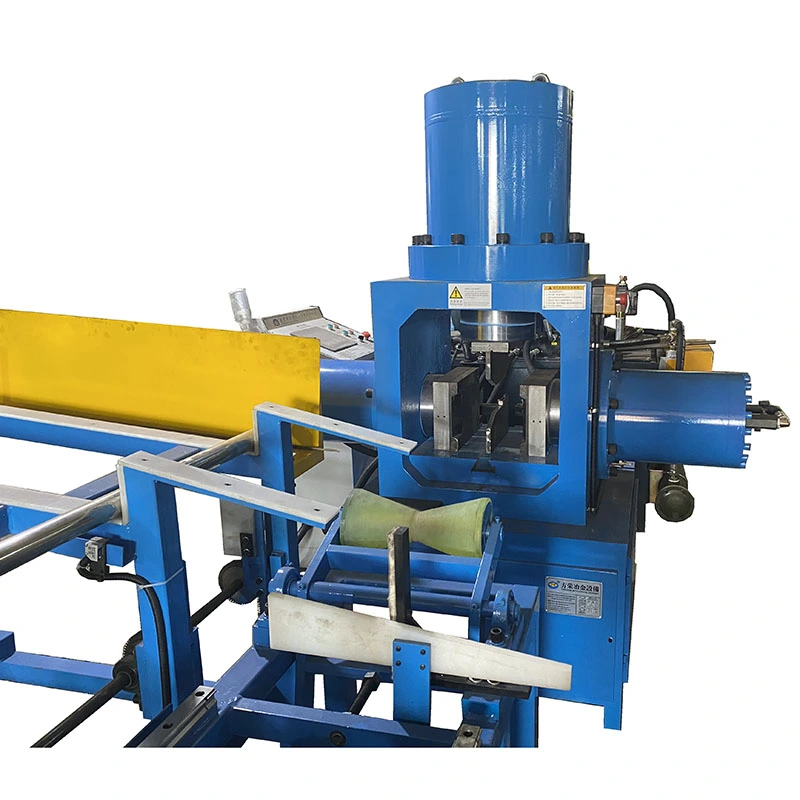
The Stainless Steel Hydraulic Three Dies Pointing Machine is designed for reducing and flattening the ends of stainless steel tubes before cold drawing, welding, forming, or assembly. Its three-die hydraulic arrangement uses two side dies and one upper die to shape the tube end in a controlled sequence.
This configuration is particularly useful when the required end profile is flattened rather than simply reduced in diameter. Instead of relying on a single pressing direction, the side dies first bring the tube into position before the upper die completes the flattening operation. This helps control deformation and maintain more consistent end dimensions from one workpiece to the next.
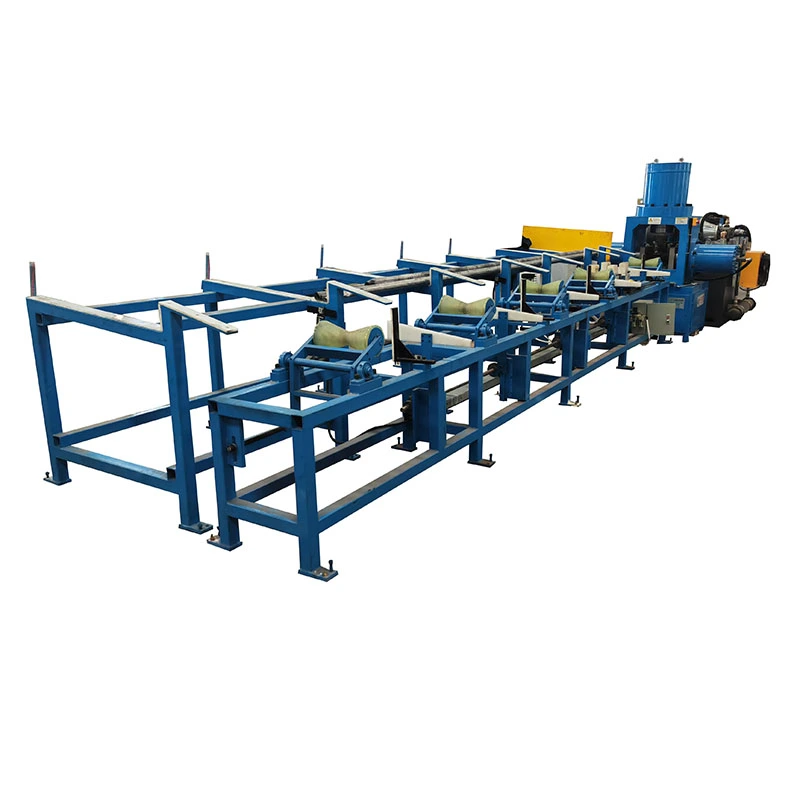
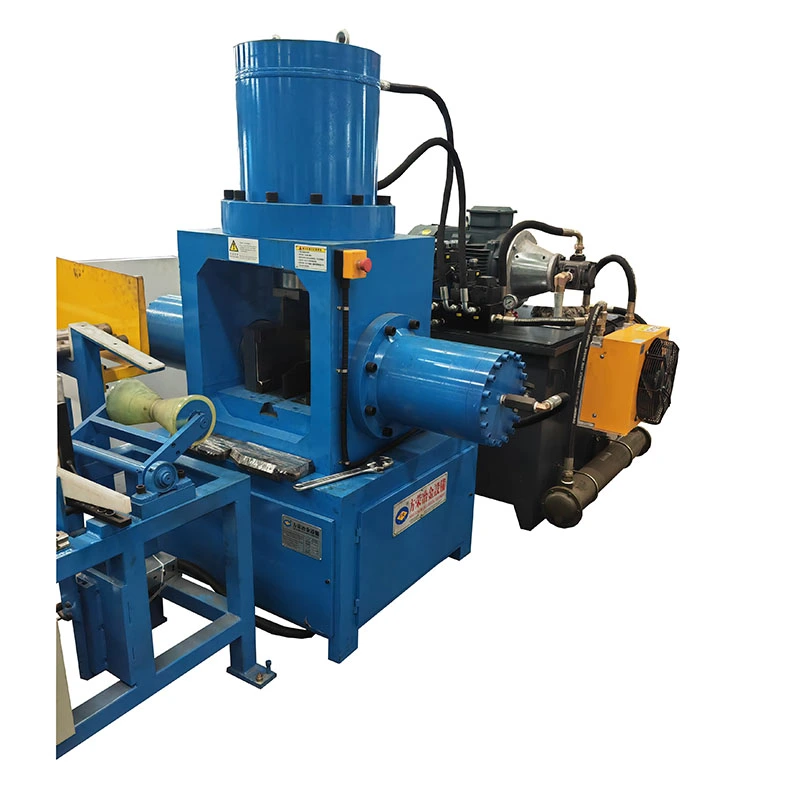
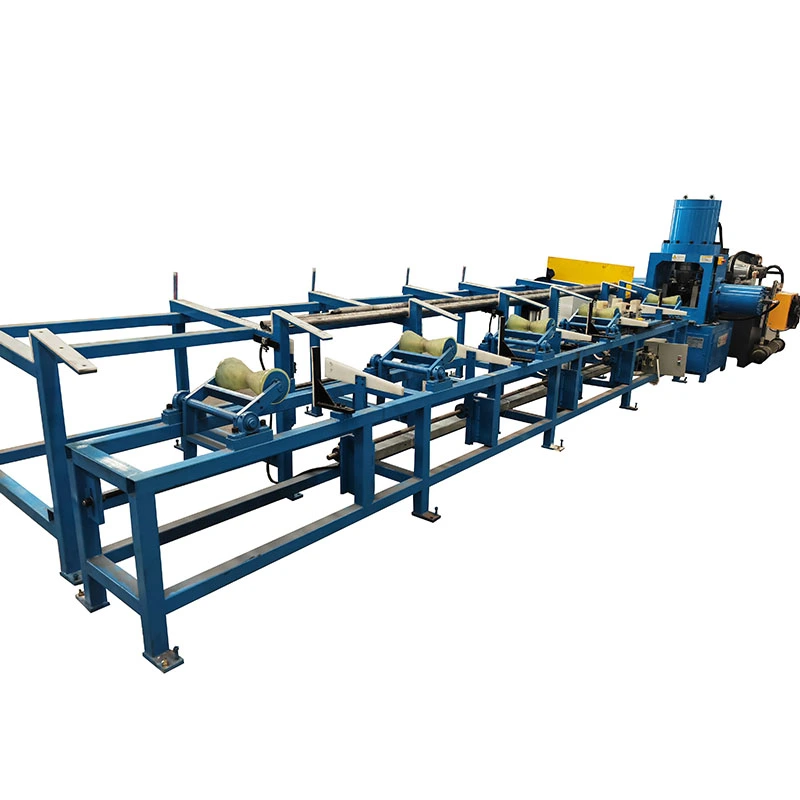
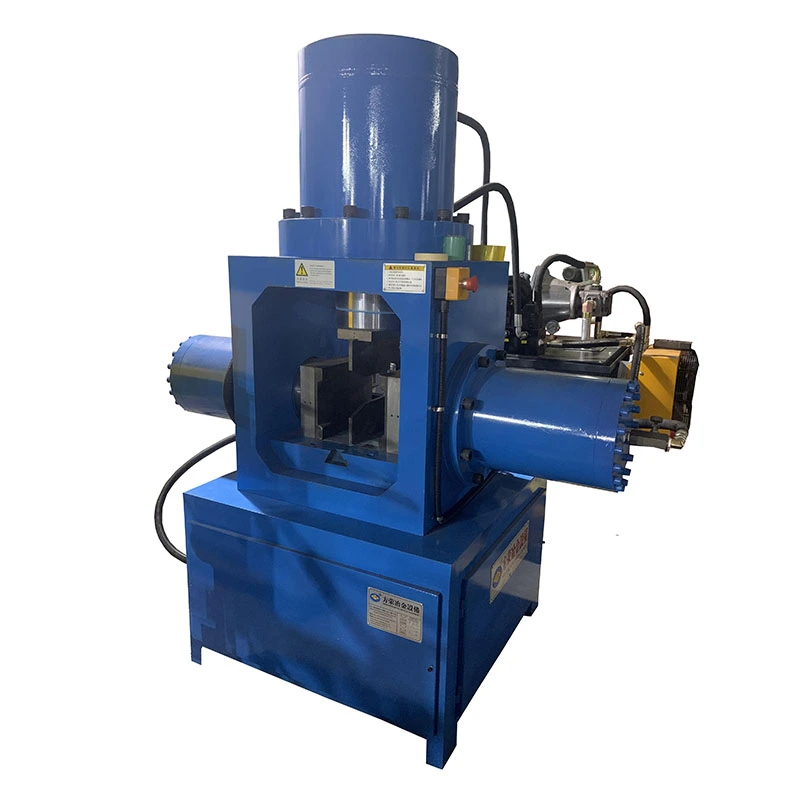
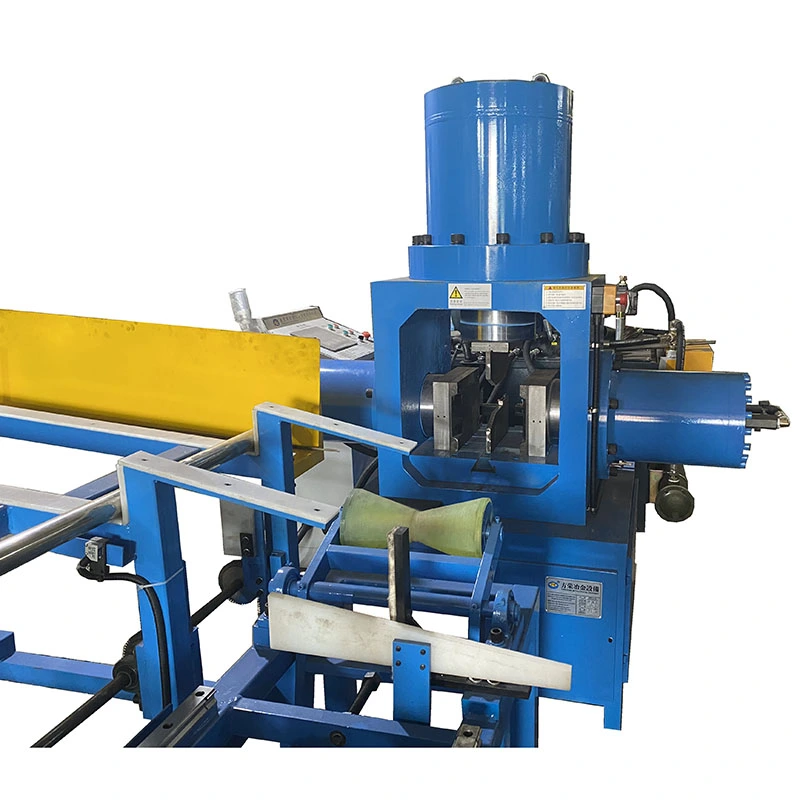
The three-die arrangement is different from machines that compress a tube from two sides or use multiple dies around the entire circumference. Here, the forming sequence is the main part of the process: the two side dies move inward first, followed by the upper die.
| Machine Configuration | Typical Forming Approach | When It Makes Sense |
| Two-die | Compression mainly from two opposing directions | Basic tube-end reduction and applications with less complex forming requirements |
| Three-die | Two side dies position and compress the tube, followed by upper-die flattening | Flattened ends, special profiles, and stainless steel tube forming where controlled deformation is required |
| Four or more dies | Forming force is distributed around more directions | Applications requiring circumferential reduction or higher control of round-section deformation |
The Stainless Steel Hydraulic Three Dies Pointing Machine is therefore not simply a smaller version of a four-die pointing machine. Its value lies in the forming sequence and the type of end geometry it is intended to produce.
The tube is positioned in the die area according to the required forming length and end dimensions. Once the cycle begins, the hydraulic cylinders execute the programmed movement rather than relying on manual pressing operations.
First, the left and right dies move toward the center and compress the tube from both sides. This brings the material into the required intermediate profile. The upper die then moves downward to complete the flattening operation.
After the forming stroke, the three dies return to their starting positions and the finished tube can be removed. The same sequence is repeated for the next workpiece.
The model should be selected from the actual tube dimensions rather than from outside diameter alone. Wall thickness, stainless steel grade, required flattened dimensions, tube length, production quantity, and downstream process all affect the required machine configuration.
| Selection Item | Why It Matters |
| Tube outside diameter | Determines the basic pointing range and die working size. |
| Wall thickness | Thicker stainless steel requires greater forming force. |
| Material grade | Different stainless steel grades can have different forming resistance. |
| Required end profile | Determines die geometry and the forming sequence required. |
| Production volume | Helps determine hydraulic capacity, automation requirements, and suitable machine size. |
| Next production process | The pointed or flattened end needs to match the requirements of drawing, welding, assembly, or further forming. |
For non-standard tube shapes, supplying a product drawing or sample is recommended. Fangrong can use the workpiece information to determine the appropriate die configuration and machine specification.
The FR-25, FR-50, FR-100, and FR-160 models cover pointing ranges from φ25 mm to φ160 mm. The listed wall thickness capacity increases from 3 mm to 12 mm as the machine size increases. Larger models use a hydraulic arrangement consisting of one upper cylinder and two side cylinders, with forming force and motor power matched to the working range.
| Parameters of Hydraulic 3 Dies Pointing Machine | ||||
| Model | FR-25 Type | FR-50 Type | FR-100 Type | FR-160 Type |
| Pointing Range | φ25 | φ50 | φ100 | φ160 |
| Thickness | 3 mm | 5 mm | 8 mm | 12 mm |
| Upper Cylinder Diameter | - | φ250 125T | φ320 200T | φ380 300T |
| Side Cylinders Diameter | - | 2 pcs φ180 65T × 2, 130T | 2 pcs φ200 100T × 2, 200T | 2 pcs φ250 125T × 2, 250T |
| Power | - | 15 kW | 20 kW | 30 kW |
Custom specifications are available according to tube dimensions, material, forming requirements, and production conditions. The specifications above are reference values, and actual parameters may vary by material type.
This Stainless Steel Hydraulic Three Dies Pointing Machine is used where the tube end needs to be changed from its original round profile into a flattened, reduced, or specially formed section. The finished end can then enter a subsequent manufacturing operation without relying on inconsistent manual preparation.
Common applications include stainless steel decorative tubes, furniture tubing, handrails and railings, door and window profiles, automotive structural tubing, architectural stainless steel products, precision tubing, and special-shaped tube production.
For manufacturers producing different tube profiles, interchangeable or customized dies can be considered according to the required end shape and dimensions.
The standard machine uses hydraulic control for the three-die forming cycle. For production lines with higher output requirements, the equipment can be configured with automatic loading and unloading systems to reduce manual handling between cycles.
Customized hydraulic force, die dimensions, machine size, control configuration, and automation can also be considered. The final configuration depends on the workpiece and the production line rather than applying one standard setup to every stainless steel tube application.
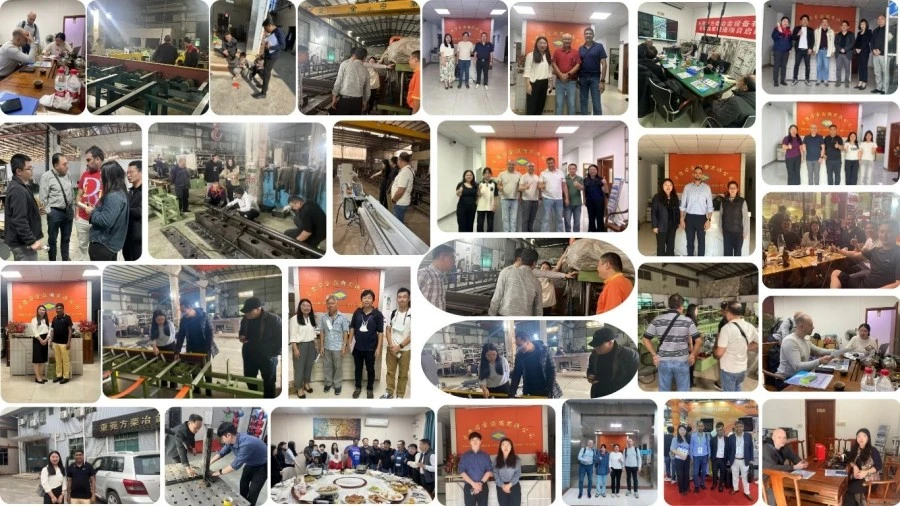
Fangrong was established in 1998 and has more than 26 years of experience in the design and manufacture of straightening machines, cold drawing equipment, and related metallurgical machinery. Its equipment is used in more than 60 industries and has been supplied to over 10,000 customers in more than 60 countries and regions.
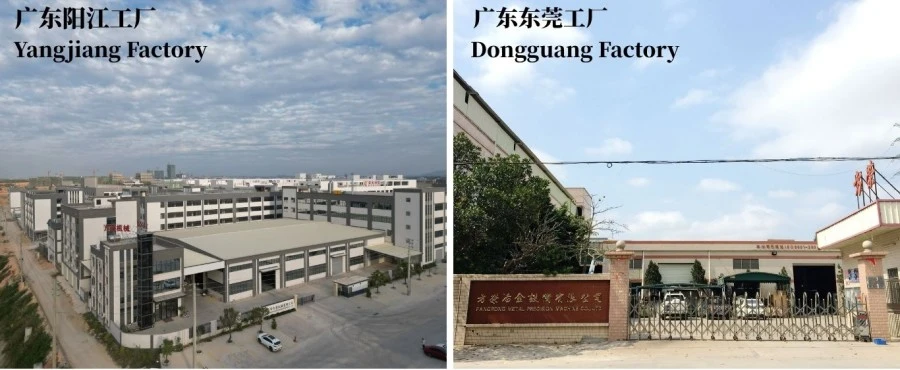
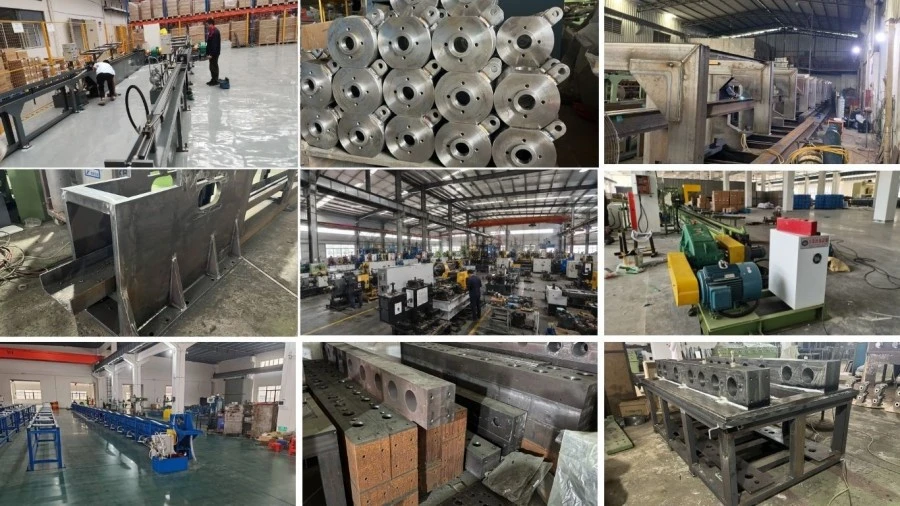
The company operates two manufacturing facilities in Guangdong Province. Dongguan Fangrong Metallurgical Equipment Co., Ltd. in Dalang Town, Dongguan City is the headquarters and primary manufacturing base, producing precision cold drawing machines, straightening machines, thread rolling equipment, and related machinery.
Yangjiang Fangrong Machinery Co., Ltd. in Yangdong District, Yangjiang City provides additional manufacturing capacity and supports equipment production and delivery.
Manufacturing begins with the workpiece requirements rather than a fixed machine configuration. Tube dimensions, forming force, die arrangement, hydraulic capacity, and control requirements are confirmed before production.
Engineering and Component Preparation
Mechanical drawings and hydraulic schematics are reviewed first. Steel plates, hydraulic components, electrical parts, cylinder components, and die materials are then prepared according to the approved configuration.
Structural Fabrication
The main frame and supporting structure are fabricated and welded before machining. Key mounting surfaces are subsequently processed to provide the required assembly accuracy.
Die and Cylinder Work
The upper and side forming components are manufactured according to the selected pointing range. Cylinder barrels, piston rods, die seats, guides, and other critical components are machined and inspected before installation.
Hydraulic and Electrical Integration
The hydraulic power unit, cylinders, valves, pipelines, control cabinet, and PLC system are connected after mechanical assembly. The three cylinders are checked through the complete forming sequence.
Machine Trial
The Stainless Steel Hydraulic Three Dies Pointing Machine is first operated without material to check movement and control functions. Test tubes can then be processed to verify the forming result, cycle operation, and response of the hydraulic system.
Final Acceptance
Mechanical movement, hydraulic operation, electrical functions, safety devices, and general assembly are checked before the machine is prepared for shipment.
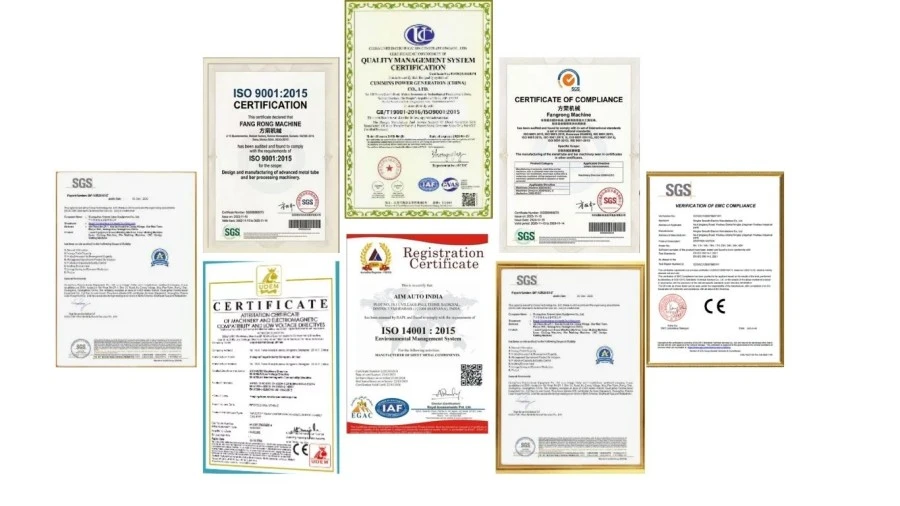
ISO9001:2015: Quality management system certification, Certificate No. UQ231211R1.
CE Mark: Equipment compliance with Machinery Directive 2006/42/EC, including safety provisions such as emergency stops, two-hand controls, and light curtains.
SGS Inspection: Independent inspection and verification can be arranged for applicable equipment orders.
Patents: Fangrong holds 32 invention patents and more than 100 utility model patents. Relevant examples include patent 2013207829011 for a chain tensioning device, 2008300532117 for a multi-strand die holder, and ZL2015 2 0842922.7 for a quick-change mandrel system.
Before shipment, the machine is checked against the confirmed model, forming range, hydraulic configuration, electrical system, and supplied accessories. Exposed machine surfaces and vulnerable components are protected according to the transportation method.
For overseas delivery, detachable components can be secured separately when required. The packing arrangement can also be adjusted for container loading and the customer's shipping conditions.
1. What is the main purpose of this Stainless Steel Hydraulic Three Dies Pointing Machine?
It is mainly used to flatten or reduce stainless steel tube ends before drawing, welding, secondary forming, or assembly.
2. How is a three-die machine different from a four-die pointing machine?
The three-die machine uses two side dies followed by an upper die, making it suitable for controlled flattening and special end profiles. Four-die machines apply force from four directions and are more commonly used where circumferential reduction and round-section control are required.
3. Can it process round and special-shaped stainless steel tubes?
Yes. The die configuration can be designed according to the tube profile and required finished-end dimensions.
4. How should I select the machine model?
Start with the tube outside diameter and wall thickness, then confirm the stainless steel grade, required flattened dimensions, tube length, production volume, and downstream process. These details determine the suitable machine and die configuration.
5. Can the dies be customized?
Yes. Customized dies are available for different flattened shapes, special profiles, and tube-end dimensions.
6. Can the machine be integrated with automatic loading and unloading?
Yes. Automatic loading and unloading can be added according to the production line layout and workpiece dimensions.
7. What information should I send for a quotation?
Please provide the tube material and grade, outside diameter, wall thickness, tube length, required end dimensions, production capacity, voltage requirement, and product drawing if available.
8. Can Fangrong test our stainless steel tubes?
Sample processing can be discussed when the forming result needs to be verified before equipment selection. Tube samples, drawings, or detailed dimensions can be provided for evaluation.
9. What is the delivery time?
Delivery depends on the machine configuration. Standard equipment is generally arranged according to the confirmed production schedule, while customized dies, automation, and special configurations may require additional time.
10. What warranty is provided?
A 12-month warranty is provided against manufacturing and quality defects. Technical support and spare parts services are available after delivery.
Address
NO.163,Shatong Road,Shabu 2nd Industrial Zone, Dalang Town, Dongguan City, Guangdong, China









