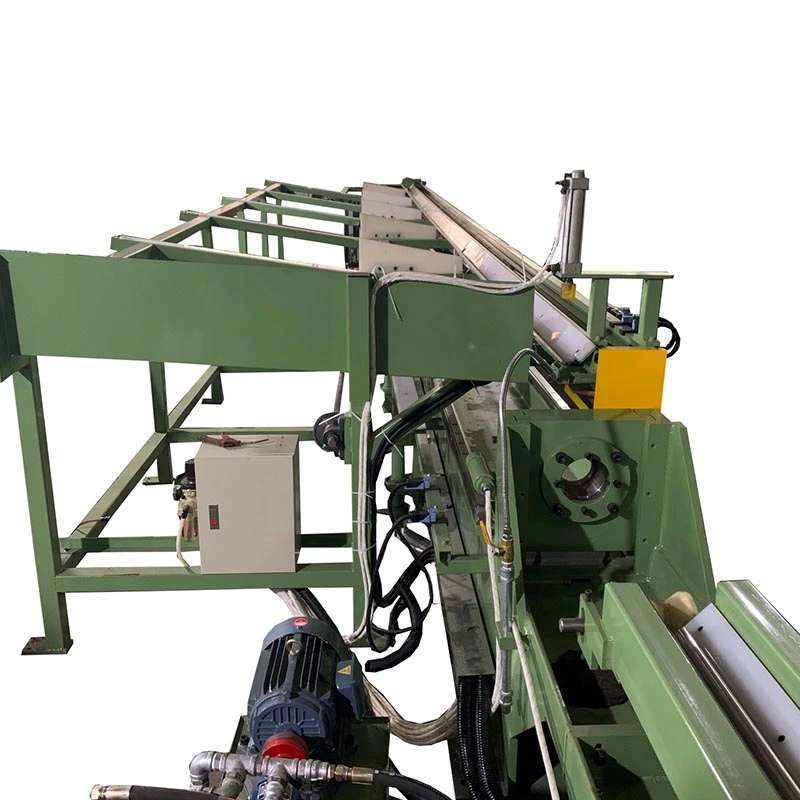
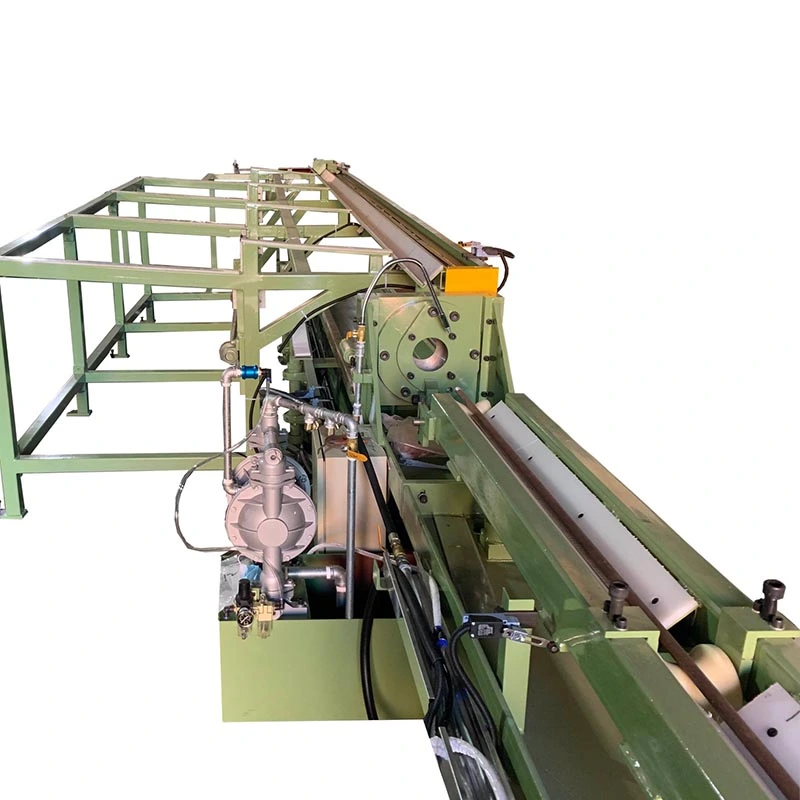
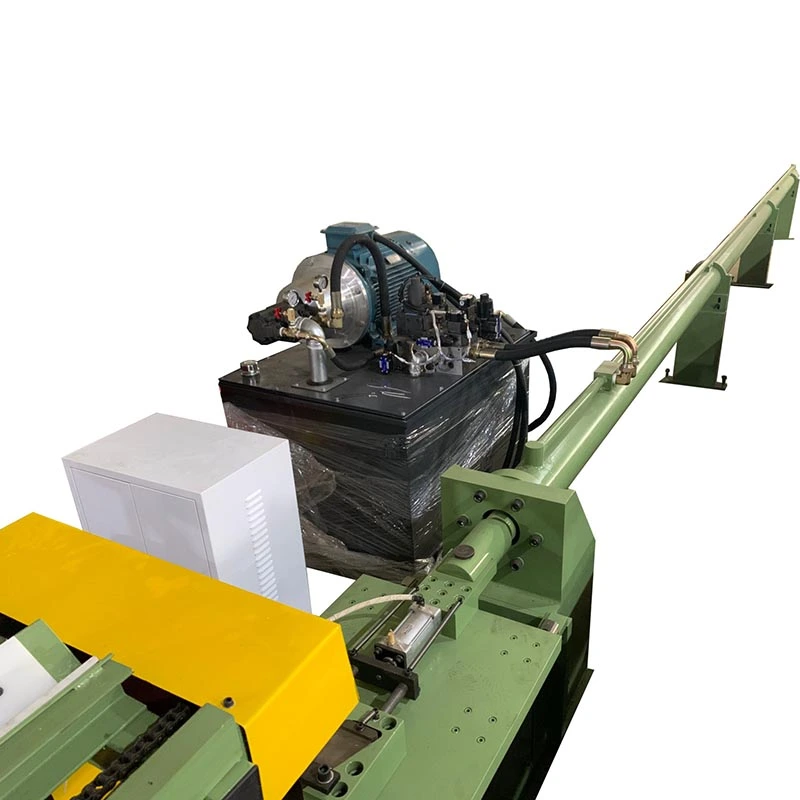
We offer a comprehensive range of precision metal processing equipment, including straightening, cold drawing, pointing, chamfering, cutting, thread rolling machines, and drawing dies, tailored for tube, bar, and wire materials across diverse industries.
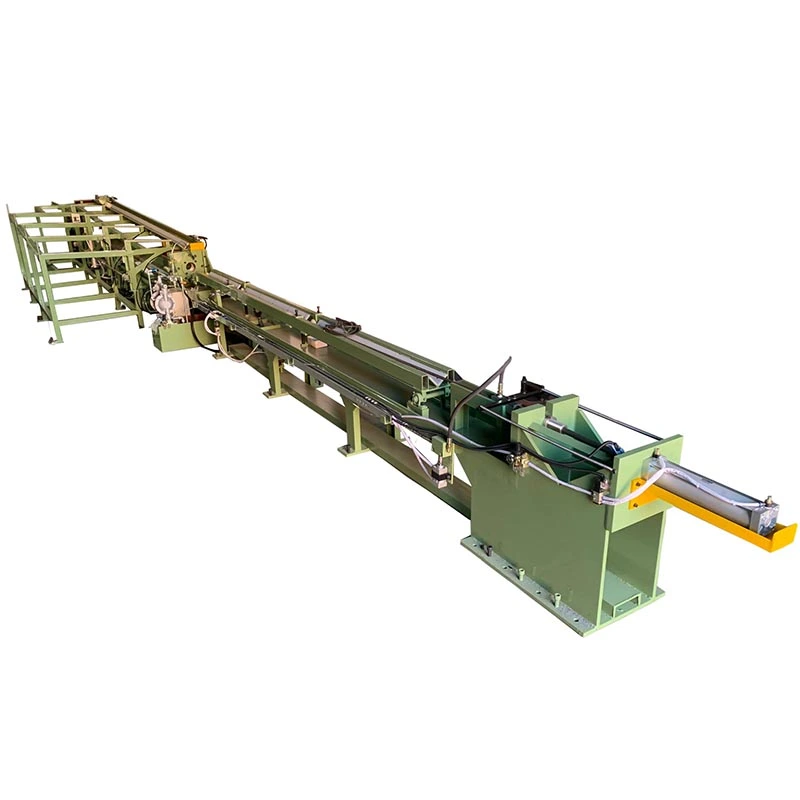
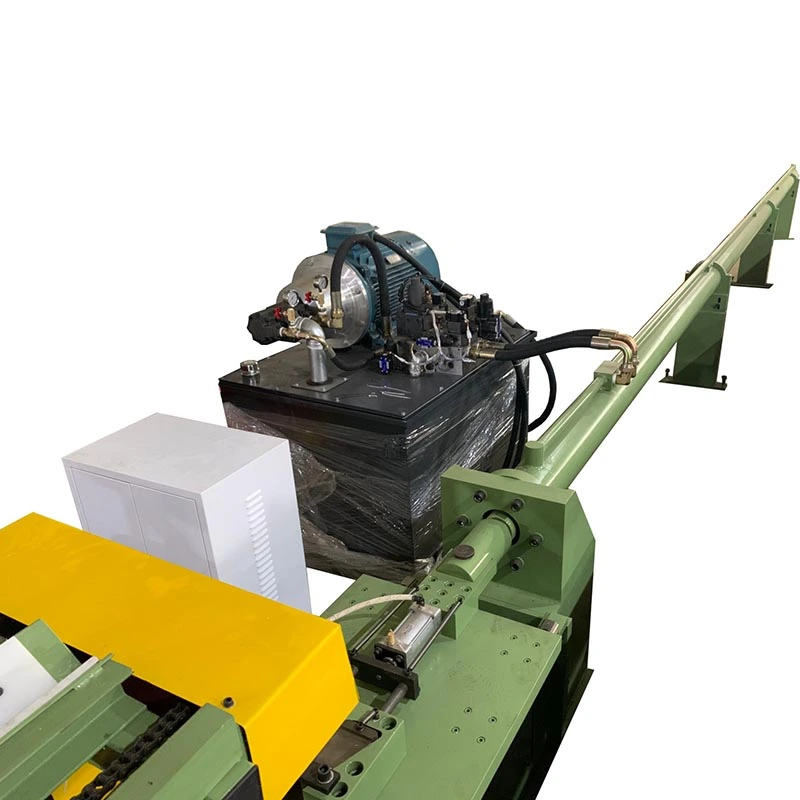
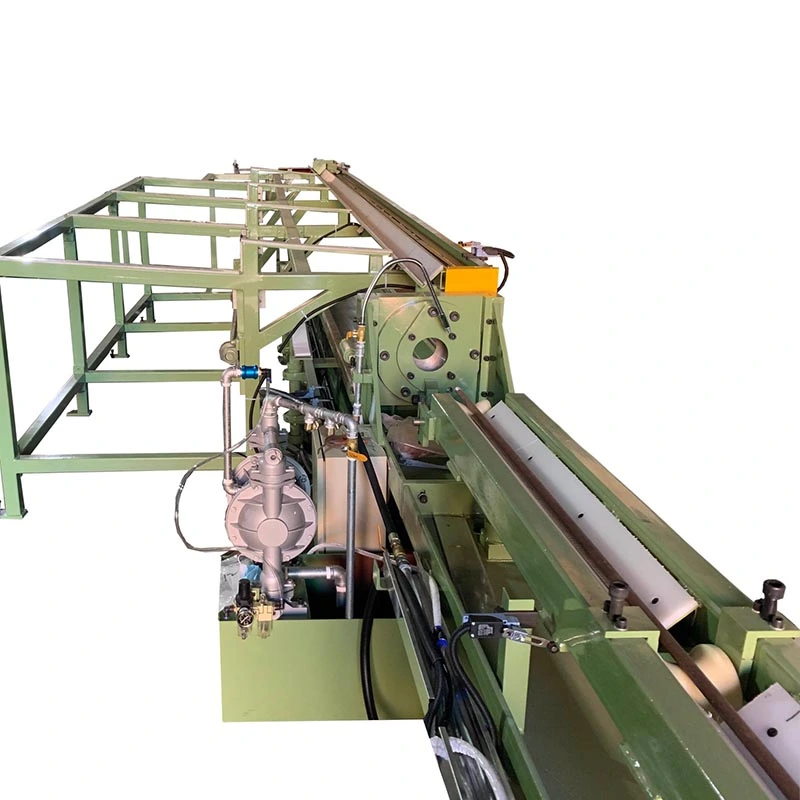
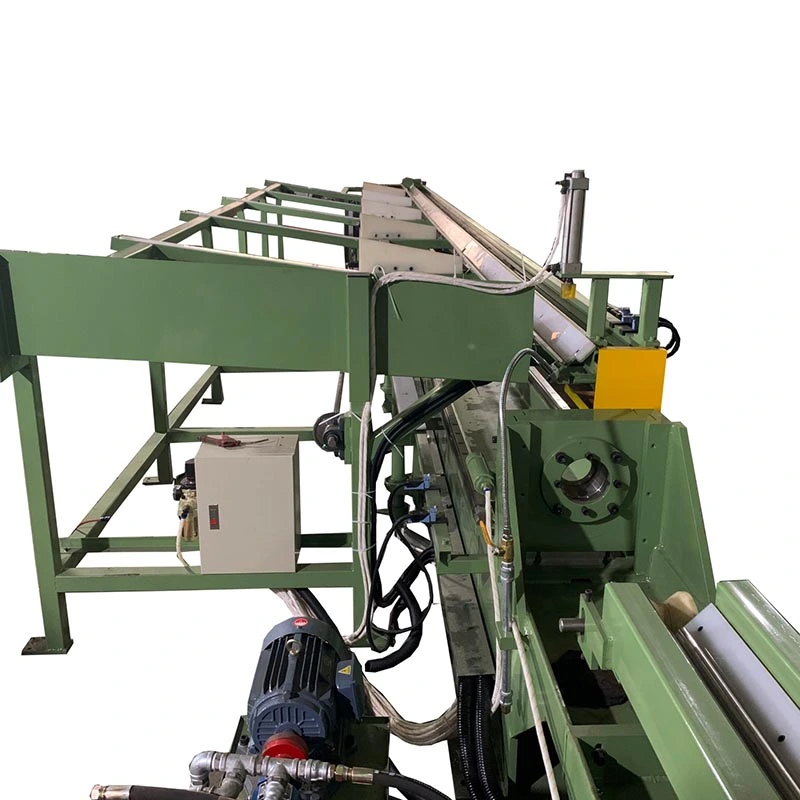
The Irregular Hydraulic Cold Drawing Machine is intended for forming complex non-round profiles that require high drawing force and controlled deformation, including square, rectangular, hexagonal, octagonal, oval, channel, angle, T-sections, and custom asymmetric shapes. A hydraulic drive provides 50–20,000 kN drawing force with strokes up to 25 m, allowing large or high-strength tubes and solid bars to be formed in a single cold drawing pass. Precision dies control profile geometry, corner definition, and dimensional accuracy, making the process suitable for steel, stainless steel, copper, aluminum, and specialty alloy sections where conventional rolling cannot achieve the required profile.
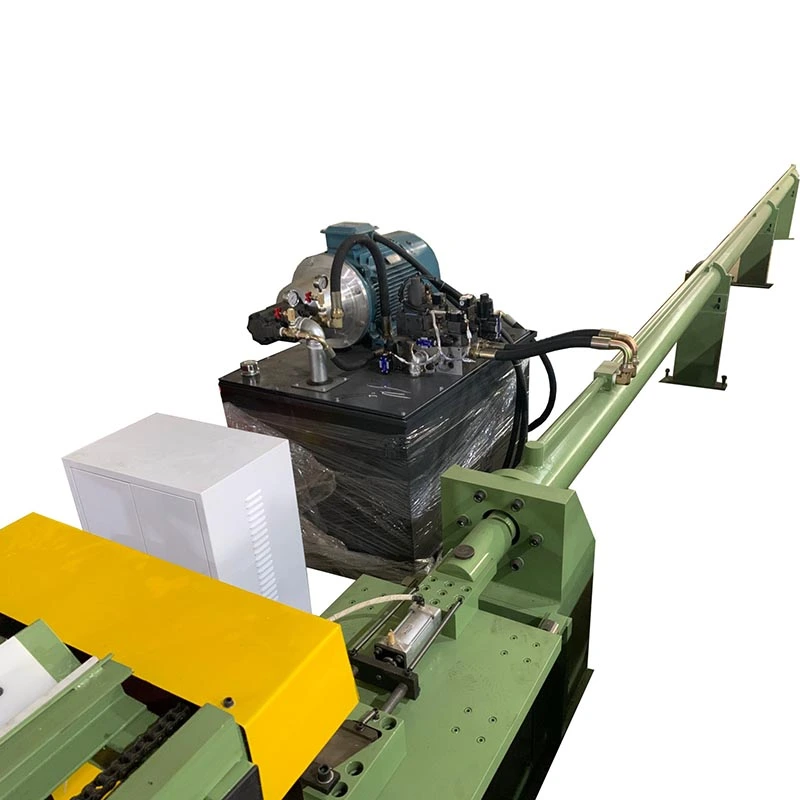
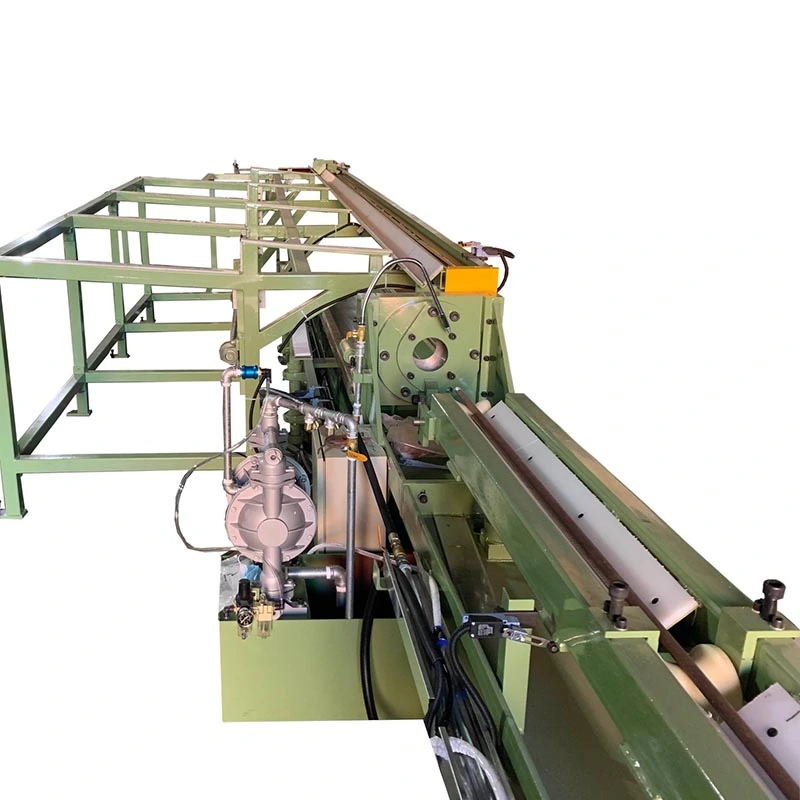
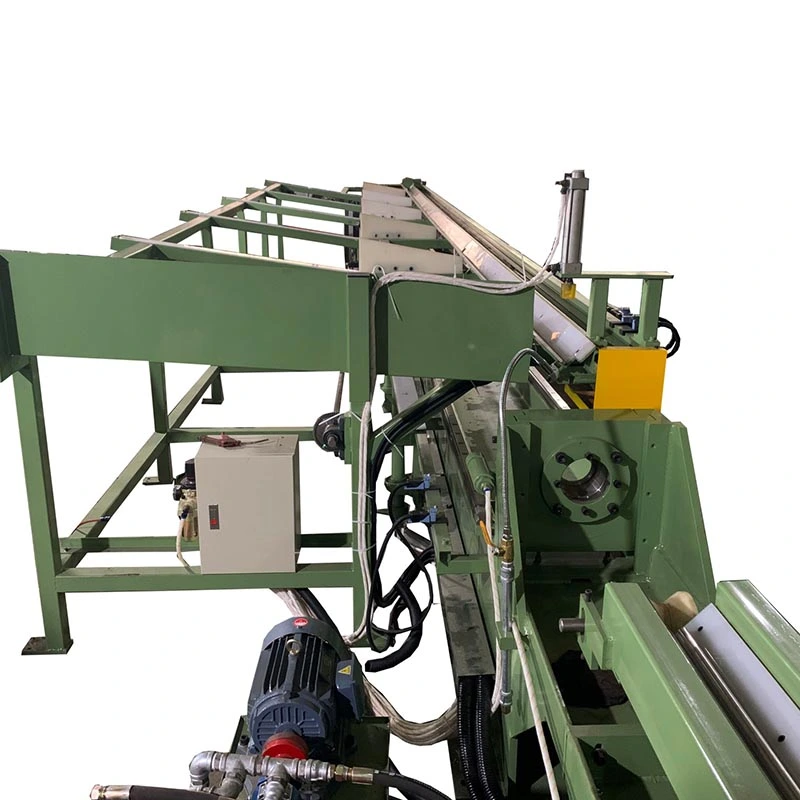
The Irregular Hydraulic Cold Drawing Machine is a hydraulically powered drawbench engineered specifically to produce non-circular metal sections---including square, rectangular, hexagonal, octagonal, oval, channel, angle, T-section, and custom asymmetric profiles---from round tube or solid bar stock through a single cold drawing pass. Unlike general-purpose drawing machines that produce round sections, this equipment incorporates specialized die systems and precision-guided carriages that maintain complex cross-sectional geometry throughout the drawing process.
The machine operates by pulling a pointed workpiece through a precision-machined die with a non-round aperture. As the material passes through the die, it plastically deforms to match the die cavity geometry---reducing cross-sectional area while simultaneously reshaping the section. For tube drawing, an internal mandrel or plug controls wall thickness distribution across the irregular section. Hydraulic power provides smooth, vibration-free force application---critical for maintaining sharp corners and consistent wall thickness in complex sections.
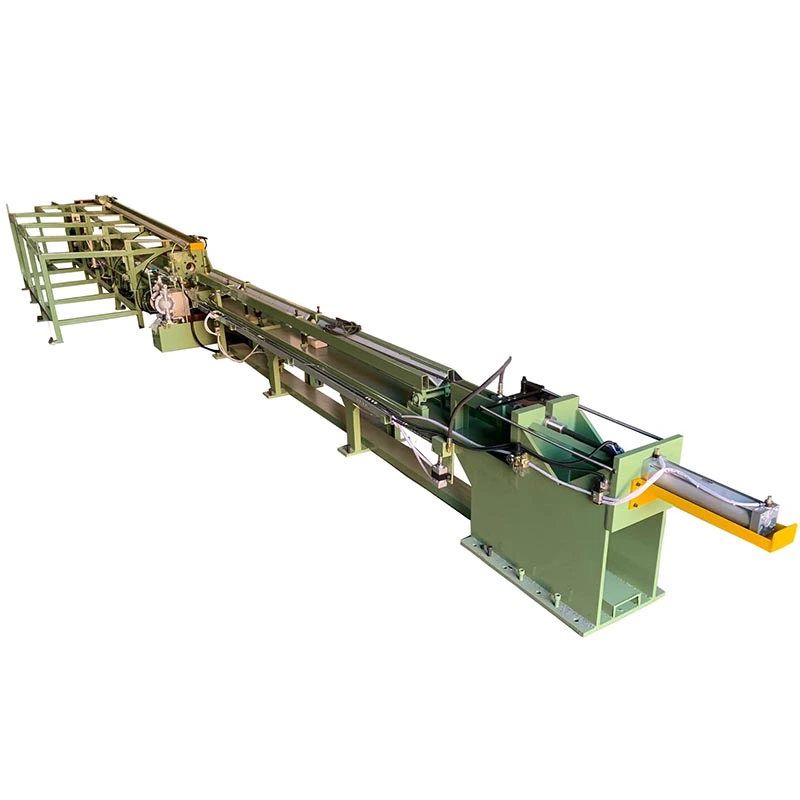
Hot-rolled or extruded non-round sections present fundamental limitations: loose dimensional tolerances (typically ±0.5mm or worse), scale-covered surfaces requiring extensive cleaning, decarburization layers that weaken surface properties, and inconsistent mechanical properties across the section. Alternative methods each have trade-offs: hot rolling cannot achieve tight tolerances on corner radii and flatness; cold roll forming is limited to uniform sections and leaves residual stresses; extrusion offers complex shapes but at significantly higher cost and lower production rates.
Cold drawing solves these constraints through a fundamentally different deformation mechanism. The combination of die geometry and controlled reduction forces the material to flow into the die cavity under compressive and tensile stresses. This produces:
- Tight dimensional control: Tolerances down to ±0.05mm on critical dimensions
- Superior surface finish: Smooth, scale-free surfaces ready for direct use
- Enhanced mechanical properties: Cold working increases yield strength and hardness while maintaining ductility
- Sharp, defined corners: Unlike hot-formed sections that exhibit rounded corners, cold-drawn profiles maintain precise corner geometry essential for structural integrity and assembly fit
- Consistent wall thickness: Uniform material distribution ensures predictable performance under load
With 26 years of cold drawing equipment manufacturing since 1998, FangRong has engineered solutions for thousands of irregular section applications. Our Irregular Hydraulic Cold Drawing Machines produce sections ranging from small precision profiles under 10mm to large structural sections exceeding 300mm, across carbon steels, alloy steels, stainless steels, aluminum, copper, titanium, and specialty alloys. Every machine incorporates engineering knowledge accumulated from 10,000+ customers across 70+ countries---including 5,000+ steel mills, 2,100+ stainless steel processors, 1,800+ copper manufacturers, 700+ aluminum producers, and 500+ titanium and specialty alloy customers.
1. Precision Non-Round Geometry Control
The prestressed frame and rigid guided carriage ensure perfect die alignment throughout the full stroke---critical for maintaining complex cross-sectional geometry. Unlike chain-type or mechanical drawbenches that can experience alignment drift, the hydraulic system maintains consistent force vector alignment. Sharp, defined corners are preserved---hot-formed sections cannot match this precision.
2. Hydraulic Power with Vibration-Free Force Delivery
Hydraulic cylinders deliver smooth, stepless force application---eliminating the chatter marks and surface defects common with mechanical or chain-driven systems. This is particularly critical for irregular sections where uneven force distribution can cause distortion, wall thickness variation, or corner rounding.
3. Wide Section Profile Capability
Supports square, rectangular, hexagonal, octagonal, oval, elliptical, channel, angle, T-section, and custom asymmetric profiles. Die changeover systems enable rapid profile switching, making the machine suitable for both high-volume production and job-shop flexibility.
4. Multi-Pass Drawing Capability
Complex sections requiring significant reduction can be drawn in multiple passes with intermediate heat treatment. Each pass progressively refines dimensions and mechanical properties. The hydraulic system maintains consistent force regardless of pass sequence.
5. Wall Thickness Control for Tubes
For tube drawing, internal mandrel or floating plug systems control wall thickness distribution across irregular sections. Critical for applications where uniform wall thickness determines pressure rating or structural performance.
6. Integrated Production Line Options
Optional in-line systems include pointing (head reduction), straightening, and cut-to-length shearing---creating a complete production line from raw stock to finished sections in a single pass.
7. Material Versatility
Processes carbon steel (low/medium/high carbon, alloy, HSLA), stainless steel, aluminum, copper, brass, titanium, nickel alloys, and specialty metals. Drawing force and speed adjustable to match material-specific deformation characteristics.
8. PLC Control with Process Data Logging
Programmable logic controller with HMI enables precise parameter programming and real-time monitoring. Data logging supports quality traceability and process optimization---essential for ISO9001-certified operations.
Selecting the correct model requires matching machine capacity to your specific production requirements. Key selection parameters include: drawing force (determined by cross-sectional area reduction and material yield strength), maximum section size (dictated by die cavity dimensions and carriage opening), stroke length (determined by finished product length), and drawing speed (affects production rate and surface finish quality). For irregular sections, the effective drawing force requirement is typically higher than for round sections of equivalent area due to the additional deformation work required to reshape corners and maintain geometry.
Our Irregular Hydraulic Cold Drawing Machines range from 50KN to 20000KN, with stroke up to 25m and speeds up to 30m/min. All specifications are customizable. For section dimensions, refer to the maximum circumscribed circle diameter---the smallest circle that encloses the irregular section.
| Model / Technology parameter | FR-2T | FR-5T | FR-10T | FR-15T | FR-20T | FR-30T | FR-50T | FR-70T |
| Max. Drawing Force(KN) | 20 | 50 | 100 | 150 | 200 | 300 | 500 | 700 |
| Drawing Speed(m/min) | 0~10 | 3~10 | 3~10 | 3~10 | 3~10 | 3~10 | 2~10 | 10~16 |
| Effective Length of Finished Pipe(m) | 6 | 5 | 5 | 9 | 5 | 5 | 7 | 9 |
| Drawn Range of Outer Diameter of Finished Pipe(mm) | φ5max | φ25max | φ50max | φ60max | φ70max | φ30~φ80 | φ30~φ100 | φ30~φ100 |
| Max. Drawn Thickness of Finished Pipe(mm) | 1.5mm | 2mm | 3mm | 4mm | 5mm | 6mm | 8mm | 10mm |
| Main Oil Cylinder(mm) | φ63*φ35 | φ80*φ45 | φ125*φ70mm*3200mm | φ125*φ70 | φ150 | φ180*φ90*3000 | φ200*φ100 | φ280*φ150*9000 |
| Number of Systemic Station | 1 | 1 | 1 | 1 | 1 | 1 | 1 | 2 |
| Working Pressure of System(Mpa) | 21 | 21 | 21 | 21 | 21 | 26 | 26 | 26 |
| Max. Pressure of System(Mpa) | 26.0 | 26.0 | 26.0 | 26.0 | 26.0 | 31.5 | 31.5 | 31.5 |
| Main Oil Pump(manual variable plunger pump) | 40 | 40 | 40 | 50 | 50 | 50 | 50 | 50 |
| Main Motor(KW) | 3.7 | 7.5 | 22 | 30 | 45 | 75 | 75 | 132*2 |
| Outline Dimensions(W×H×L)(m) | 1.6*1.4*30 | 1.6*1.4*30 | 1.6*1.4*30 | 1.6*1.4*30 | 1.6*1.4*30 | 1.1*1.2*20 | 1.2*1.3*25 | 1.3*1.4*25 |
| Weight(t) | 2 | 3 | 5 | 8 | 10 | 15 | 20 | 30 |
Custom specifications available upon request. Section size refers to maximum circumscribed circle diameter.
- Chassis components, roll cages, suspension parts: Square and rectangular sections with tight corner radii for structural integrity
- Steering columns, driveshafts: Hexagonal and spline profiles requiring precise dimensional control
- Battery cooling tubes: Oval and rectangular thin-wall sections with uniform wall thickness for thermal management
Case: A Tier 1 automotive supplier replaced hot-rolled rectangular tubes with cold-drawn sections on a suspension component. Dimensional tolerance improved, eliminating a secondary milling operation. Production cost reduced.
- Guide rails, conveyor components: Precision square and rectangular bars for linear motion systems
- Machine frames, hydraulic linears: Heavy-wall rectangular and custom sections for load-bearing applications
- Telescopic components: Nested square and rectangular sections with controlled clearance
Case: A hydraulic cylinder manufacturer draws 80×80mm square tubes from 89mm OD rounds for cylinder bodies. Surface finish eliminates honing, saving 15 minutes of machining per cylinder.
- Trailer frames, racking systems: High-strength rectangular and channel sections
- Aircraft structural members: Titanium and alloy steel irregular sections with strict dimensional and mechanical property requirements
- Cargo container components: Standardized square and rectangular sections
- Industrial-style furniture: Precise geometric sections requiring aesthetic surface quality
- Office and retail displays: Decorative profiles with custom cross-sections
- Heat exchanger tubes: Oval and flattened tubes for enhanced heat transfer surface area
- Wind turbine components: Structural sections with high strength-to-weight ratios
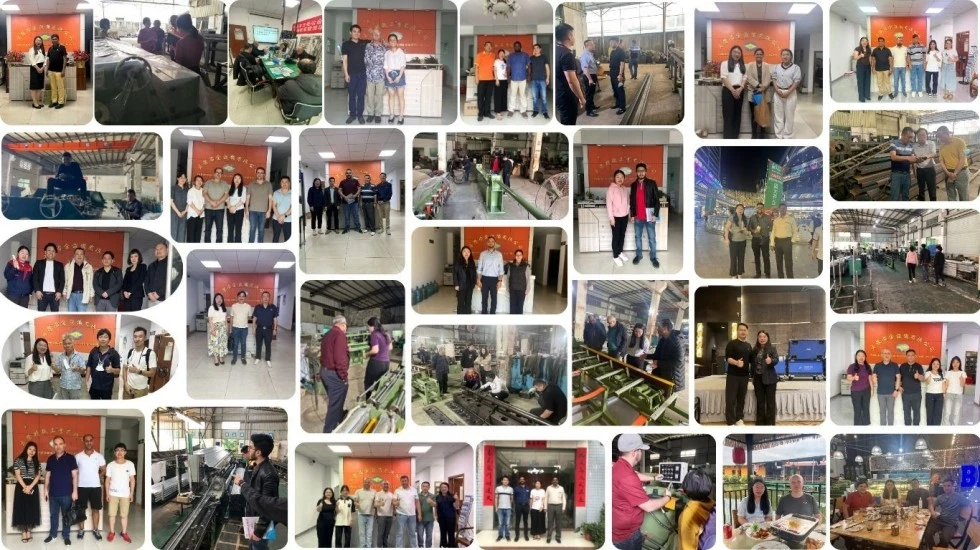
FangRong was founded in 1998 and has specialized in cold drawing equipment for 26 years. The company originated from a Joint Venture partnership with a Taiwanese manufacturer with over 30 years of brand cold drawing machine experience, transitioning to wholly-owned operation in 2013. This engineering lineage means our machines embody decades of cold drawing process knowledge---not just mechanical design, but the metallurgical understanding of how different materials behave under deformation.
Two factories: Dongguan Fangrong Metallurgical Equipment Co., Ltd. and Yangjiang Fangrong Machinery Co., Ltd. Annual production capacity: 650+ machines. Average annual turnover: 45 million RMB. Dual-facility operations enable parallel production and faster delivery.
Exported to 70+ countries. 10,000+ customers: 5,000+ steel mills, 2,100+ stainless steel processors, 1,800+ copper manufacturers, 700+ aluminum producers, 500+ titanium and specialty alloy customers. This scale provides engineering feedback that no small-scale manufacturer can match.
Every Irregular Hydraulic Cold Drawing Machine undergoes full-load testing before shipment: idle operation for 30 minutes, then progressive loading to rated capacity. Dimensional verification to ±0.02mm. Oil temperature monitored---must not exceed 60℃ under full load. Hydraulic system pressure-tested for leak-free operation.
Installation, commissioning, operator training, maintenance, and repair services. Global service partner network for local support and spare parts.
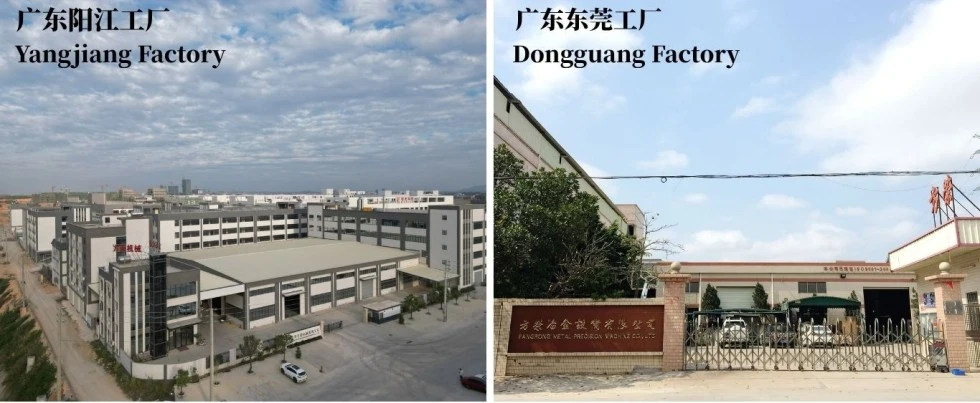
Dongguan Fangrong Metallurgical Equipment Co., Ltd. -- Headquarters and primary manufacturing base in Dalang Town, Dongguan City. Specializes in cold drawing machines, straightening machines, and thread rolling equipment.
Yangjiang Fangrong Machinery Co., Ltd. -- Secondary facility in Yangdong District, Yangjiang City, expanding production capacity and enabling faster delivery.
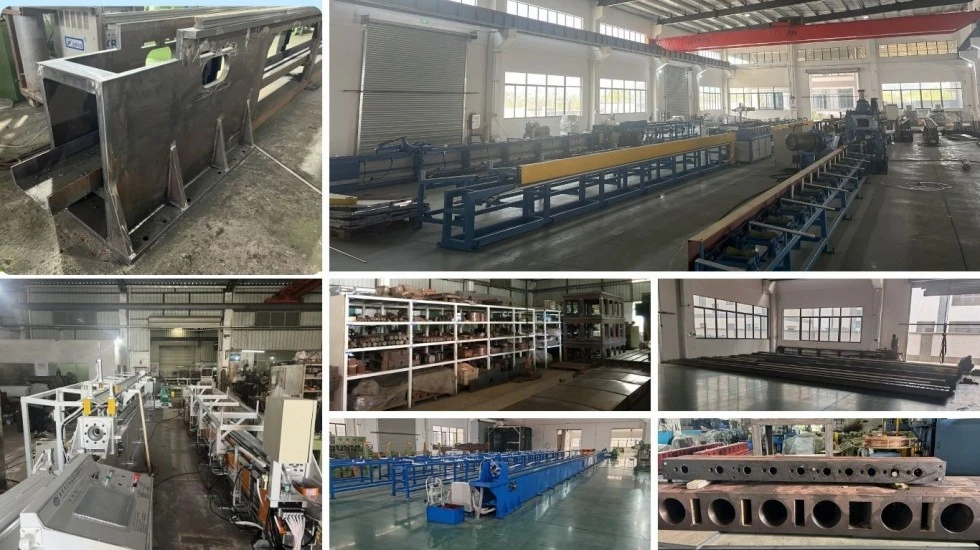
1. Order & Engineering -- Each machine engineered to customer-specific section requirements, materials, and production targets.
2. Material Procurement & Inspection -- All raw materials from qualified suppliers with incoming inspection.
3. Precision Machining -- Critical components: main cylinder, draw carriage, die holder, prestressed frame, guide rails. Guide rail straightness ≤0.5mm over full length.
4. Hydraulic System Assembly -- Power units, cartridge valve integrated blocks, control systems assembled and tested.
5. Sub-Assembly -- Feed mechanism, clamping system, optional straightening and cutting units.
6. Final Assembly -- Mechanical, hydraulic, and electrical systems integrated.
7. PLC & Control Integration -- Programming and HMI interface installation.
8. Full-Load Testing -- Every machine: idle operation 30 min, progressive loading to rated capacity, dimensional verification, oil temperature monitoring (≤60℃).
9. Quality Inspection -- ISO9001:2015 compliance verification.
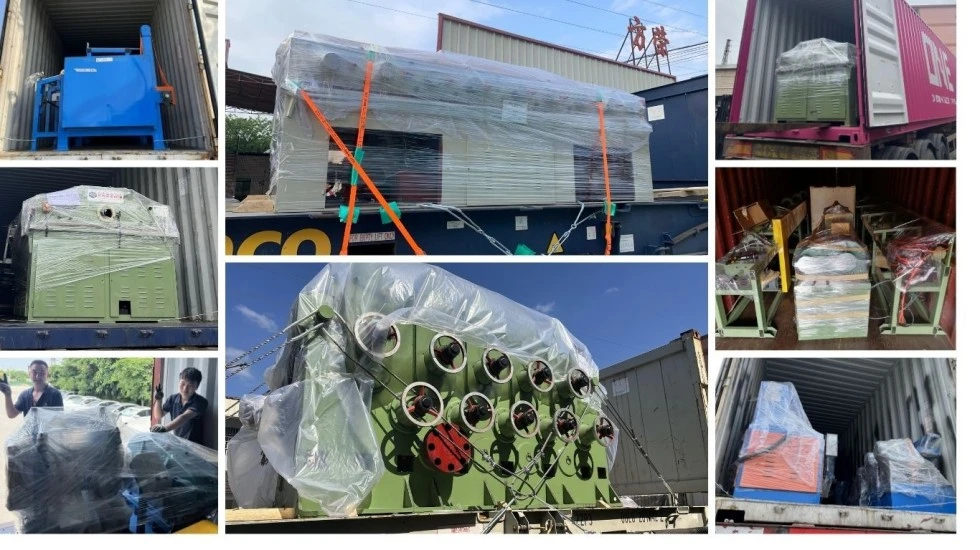
10. Packaging & Shipment -- Secure packaging for international shipping with export documentation.
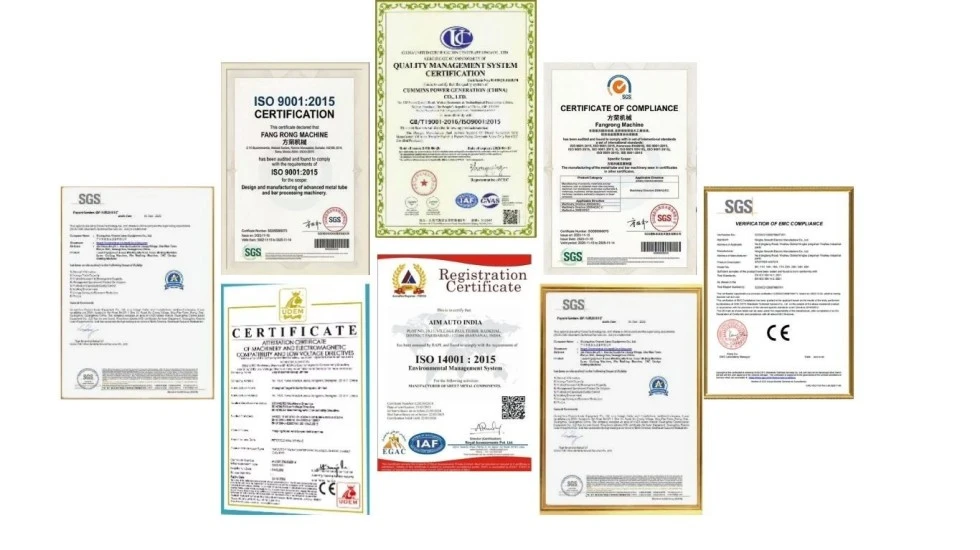
ISO9001:2015 Quality Management System -- Certificate No.: UQ231211R1. Covers design, procurement, manufacturing, and after-sales service.
CE Certification -- Complies with European Machinery Directive 2006/42/EC. Includes two-hand controls, safety light curtains, interlocked guards.
SGS Certification -- Independent verification of product quality and manufacturing processes.
National Patents -- 32 invention patents + 100+ utility model patents protecting proprietary technologies in hydraulic systems, die design, automation control, and machine structure. Representative: 2013207829011, 2008300532117, ZL2015 2 0842922.7.
Square, rectangular, hexagonal, octagonal, oval, elliptical, channel, angle, T-section, and custom asymmetric profiles. Die changeover enables rapid switching between profiles. For tube sections, internal mandrels control wall thickness distribution.
Cold drawing achieves tolerances down to ±0.05mm on critical dimensions. Sharp corners are maintained---hot-formed sections cannot match this precision.
Carbon steel (low/medium/high carbon, alloy, HSLA), stainless steel, aluminum, copper, brass, titanium, nickel alloys, and specialty metals.
| Aspect | Cold Drawing | Hot Rolling |
| Dimensional tolerance | ±0.05mm | ±0.5mm |
| Surface finish | Scale-free | Scale present, requires cleaning |
| Corner geometry | Sharp, defined | Rounded |
| Mechanical properties | Enhanced via work hardening | As-rolled, lower strength |
| Decarburization | Removed by surface shear | Present, must be machined off |
Required force = cross-sectional area reduction × material yield strength × deformation factor (1.2--1.5 for irregular sections). We provide free force calculations with your material specifications and target dimensions. For irregular sections, the deformation factor is higher than for rounds due to corner-forming work.
Typically 15--30% area reduction per pass for irregular sections. Multiple passes with intermediate annealing may be required for larger reductions. We recommend process trials with your specific material and section geometry.
Yes. The workpiece end must be reduced in diameter to pass through the die. FangRong offers integrated pointing (head reducing) machines as part of the production line.
Standard Irregular Hydraulic Cold Drawing Machines: 30--60 days. Custom-engineered machines: 90--120 days depending on specifications. Dual-factory operations enable parallel production for multiple orders.
380V, 50--60Hz power. Concrete foundation required---prestressed frame design means the foundation only supports machine weight, not drawing forces (forces are contained within the closed frame structure). Minimum floor space: depends on stroke length. We provide foundation drawings with the quotation.
Yes. Our engineering team provides die design recommendations, pass sequence planning, lubrication selection, and trial run support during commissioning. With 10,000+ customers across 70+ countries, we have encountered and solved virtually every irregular section drawing challenge.
Machine, hydraulic power unit, PLC control system with HMI, standard die holder, one set of startup tooling, installation supervision, commissioning, and operator training. Dies for your specific profiles are quoted separately based on geometry and material.
Standard: 30% deposit, 70% prior to shipment.
12 months from commissioning.
10,000+ customers across 70+ countries. We can provide industry-specific references upon request.
Submit: material type and grade, starting section dimensions, target finished section drawing, target production volume (pieces/day or tons/day), and maximum finished length. We will respond with force calculation, model recommendation, pricing, and delivery schedule.
Address
NO.163,Shatong Road,Shabu 2nd Industrial Zone, Dalang Town, Dongguan City, Guangdong, China